
Roller shutter quality inspection at delivery helps your receiving team identify missing parts, configuration differences and visible damage before installation starts. For a bulk aluminum shutter order, a correct pallet count is only the first check. Each curtain, guide rail set and motor package must also match its intended opening.
Use this guide to build a receiving record for your own purchase order. Agree the acceptance criteria, inspection scope and reporting procedure with the supplier before dispatch. A delivery check does not replace factory testing or the completed door’s commissioning.
Contents
- 1 Set the scope of roller shutter quality inspection
- 2 Check packages and quantities before separating the shipment
- 3 Match the delivered configuration to the approved door schedule
- 4 Inspect visible condition without masking damage
- 5 Define the inspection coverage before drawing conclusions
- 6 Record discrepancies and control release for installation
- 7 Discuss the receiving requirements before placing your order
Set the scope of roller shutter quality inspection
Collect the approved order, final door schedule, packing list and current drawings in one place. Add the agreed finish reference, component specifications and any inspection documents required by the contract. Check revision numbers: a receiving team working from an early quotation can report a planned change as a defect.
Assign a person to record findings and a separate, named contact who can approve a disposition. Define what the team may release for installation and what requires supplier review. Roller shutter quality inspection should leave a clear status for each opening, rather than one general comment for the whole shipment.
Keep factory evidence with the receiving file. Our aluminum shutter manufacturing guide explains the earlier production stages; this article focuses on what arrives at your site.
Check packages and quantities before separating the shipment
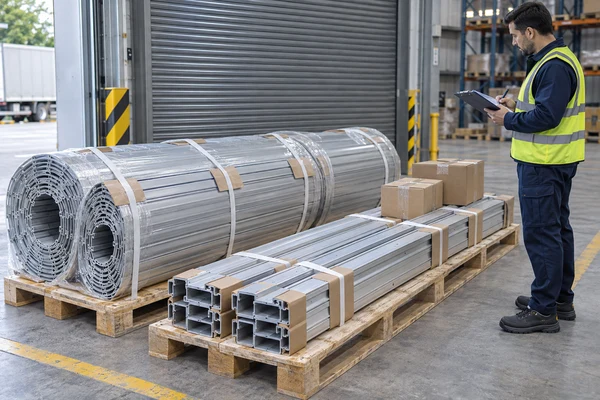
Photograph the shipment as received, including package identification and any torn wrapping, crushed corners or moisture marks. Record visible exceptions promptly through the agreed delivery procedure. Follow the applicable supplier and carrier instructions for reporting and retaining packaging; do not assume one universal claim deadline.
Reconcile package numbers with the packing list, then count the contents as unpacking proceeds. Ten packages do not necessarily mean ten complete doors. A curtain may travel separately from its guides, shaft assembly and controls. Record partial deliveries explicitly so the installation team does not search for items scheduled for a later shipment.
For bulk roller shutter orders, keep parts grouped by opening ID wherever practical. If several openings share the same size but use different motors or controls, a visual size match is not enough. Put the opening ID on the receiving record and maintain that link when moving parts into storage.
A useful roller shutter delivery checklist includes the package count, component count, identity, visible condition and any items still unavailable for inspection. Mark an unopened carton as unchecked rather than passed.
Match the delivered configuration to the approved door schedule
Roller shutter quality inspection should compare specific items with specific documents. Use accessible labels and agreed measurement points. Distinguish the building opening size from curtain width, guide length and overall assembly dimensions. These are different measurements, and each needs the correct drawing reference.
| Check | Record against the order |
|---|---|
| Curtain and bottom bar | Opening ID, specified slat profile, finish, ordered dimensions and bottom-bar arrangement. |
| Guides and supports | Correct guide set, orientation and specified brackets or mounting parts. |
| Motor and controls | Model and electrical nameplate details against the approved configuration; identify any unexplained substitution. |
| Safety and operating accessories | Quantity and model of the devices actually included in the order, plus the applicable instructions. |
| Documents and labels | Packing references, drawing revision, identification and agreed inspection or product documents. |
Do not accept a different motor simply because its stated power looks similar. Ask the supplier to confirm compatibility and the effect of the substitution on the agreed assembly. Likewise, the presence of a sensor in a carton does not demonstrate that the installed safety system works.
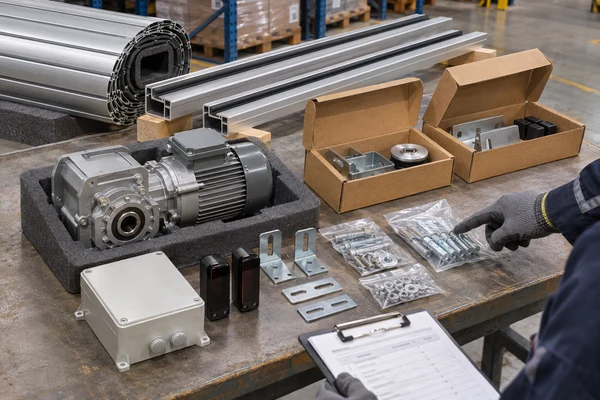
For aluminum roller shutter doors, material, construction and finish must match the selected specification. Review the aluminum roller shutter product range when defining that specification, then use the approved project documents as the receiving reference.
Inspect visible condition without masking damage
Examine accessible slat faces and edges for dents, scratches, coating damage and distorted connections. Check guides for visible bends or crushed ends, and inspect the bottom bar and supplied housings for damage. Use suitable lighting and photograph the affected area before attempting any cleaning or correction.
Roller shutter quality inspection needs enough detail for another person to find the same defect. Capture a whole-component view, the package or opening ID, and a close-up with a scale where useful. Keep the original photos. A close-up alone can show a scratch clearly while leaving its location uncertain.
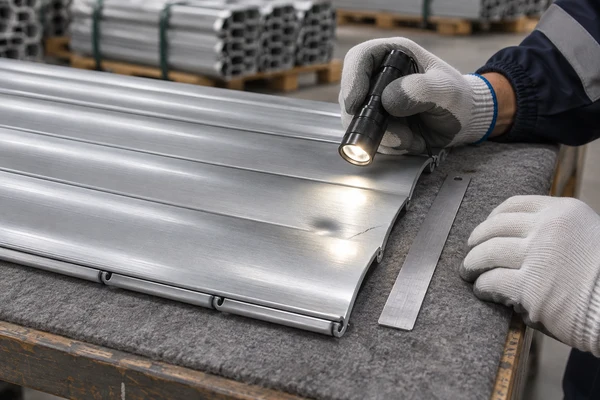
Compare appearance with the agreed finish reference and viewing conditions. Protective film, reflections and packaging residue can affect what a photograph shows. If the result is unclear, record the observation and ask for review instead of inventing a tolerance or removing the evidence.
Roller shutter shipping damage may become apparent only after unpacking. Keep relevant packaging and record when and where you found it. As a manufacturer-specific example, the freight-receiving section of Cornell’s TruCycle installation instructions calls for damage checks and manufacturer authorization before proceeding with damaged components. Apply the instructions and terms for your supplied door, rather than copying another manufacturer’s deadlines or liability terms.
Define the inspection coverage before drawing conclusions
A roller shutter quality inspection plan should state which checks cover every package or opening and which use an agreed sample. Specify how the sample is chosen, what constitutes a defect and what happens when a sample fails. Do not choose a convenient percentage on arrival and treat it as an established acceptance standard.
For a mixed order, record the actual configurations examined. Checking several identical shutters gives no direct evidence about a different profile, motor arrangement or finish elsewhere in the batch. If a defect suggests a wider issue, agree the expanded inspection with the responsible parties and document the additional scope.
Keep receiving checks within the available equipment and competence. Do not energize loose motors, adjust spring assemblies or run an unsecured curtain to produce a pass result. Operational and safety checks belong in the approved installation and commissioning procedure. The aluminum shutter installation guide covers that later handover.
Record discrepancies and control release for installation
Create one roller shutter inspection report that links the order, shipment and individual openings. For each discrepancy, record the component, expected requirement, observed condition, photo references, inspector and date. Add the responsible contact, agreed action and current status.
For example, if opening A-03 has a bent guide, identify that guide and hold the affected set for review. Do not quietly borrow a guide from A-04 unless the supplier confirms compatibility and the records show the transfer. This is an illustrative receiving example, not a reported customer case.
Separate unchecked, accepted and held items in the records and, where practical, in storage. Protect components according to their handling and storage instructions. A delivery signature, a warehouse receipt and technical acceptance serve different purposes; make the status visible to the people scheduling installation.
Close each nonconformance record only after documenting the agreed resolution and checking the replacement or corrected item. Retain the original finding alongside the closure evidence. Roller shutter quality inspection is complete for receiving purposes when the inspection scope and outstanding items are clear, even if a separate installation release remains pending.
Discuss the receiving requirements before placing your order
SEPPES supplies industrial door products through FastDoorChina. For a new aluminum shutter project, send the opening schedule, required configuration, destination and proposed receiving checks. Identify the documents and package markings your team needs to keep a bulk shipment traceable.
Use the form below or contact SEPPES about your shutter order to discuss those requirements. Agree the roller shutter quality inspection criteria in the order documents so the supplier, receiving team and installer work from the same reference.


